 86-539-3101518
Fax: 86-539-3101518
Mobile: +86-15969943322
+86-18853986768
Email: Jasonqiao@sdfocusmachinery.com
Factory address: No.1 Zhubao wood industry zone, Lanshan district, Linyi-276000, Shandong,China.
Office: F16, Amethyst mansion, Linyi, Shandong,China.
Time: 2026-10-19 10:50
Description:

 Jasonqiao@sdfocusmachinery.com
Product Details
Brief Guide to OSB/PB Production
Overview of the Manufacturing Process
1 · Flake Preparation Section
Raw wood material is delivered to the factory and sorted by species.
Option 1:
Wood logs, offcuts, and other short pieces are fed via a conveyor belt into a drum chipper. The resulting wood chips are transported—via a discharge conveyor and a bucket elevator—to a storage silo. These chips are then processed into high-quality flakes using a ring flaker and pneumatically conveyed to a wet flake silo.
Option 2:
Raw wood material is fed via a conveyor into a long-log flaker, where it is processed directly into high-quality flakes in a single pass. The flakes are then pneumatically conveyed to a wet flake silo.
Option 3:
Long-log timber (such as small-diameter wood) is fed via a conveyor into a long-log flaker, where it is processed directly into high-quality flakes. The flakes are then pneumatically conveyed to a wet flake silo. Alternatively, wood logs, offcuts, and other short pieces are fed into a drum chipper; the resulting chips are pneumatically conveyed to an intermediate storage silo, then processed into high-quality flakes using a ring flaker, and finally pneumatically conveyed to a wet flake silo. 2 · Drying and Screening Section
Wood chips (shavings) exiting the wet-material bin are transported via a screw conveyor into a rotary dryer. Once dried, the material is moved by another screw conveyor to a screening machine. The dryer’s discharge screw conveyor is equipped with a spark detection system; if an alarm is triggered, the dry material can be automatically ejected from the system. Oversized chips are sent to a secondary crusher for further processing, then—along with the medium-sized chips—are transported by a screw conveyor to an air-flow classifier (sorter). Properly sized fine material is sent to the chip storage bin. Material that passes through the air-flow classifier is directed to a chip bin for intermediate storage. Oversized material separated by the classifier is sent to a mill for further size reduction, then combined with the fine chips and routed to the chip storage bin. Depending on the required ratio of surface-layer to core-layer chips—which varies based on the thickness of the panels being produced—a portion of the coarse chips can be diverted to a grinding machine (refiner) to be processed into surface-layer material.
3 · Gluing Section
This section encompasses the preparation and delivery of paraffin emulsion and hardener solutions, the storage of additives, and a system for preparing and applying the adhesive mixture. Adhesive mixtures for the surface and core layers are prepared in a centralized glue-mixing unit. The entire glue preparation and application system is managed via a PLC-based control system. Automatic measurement, continuous proportioning, quantitative application, and adjustment can be implemented in accordance with process specifications.
4 · Sizing Section
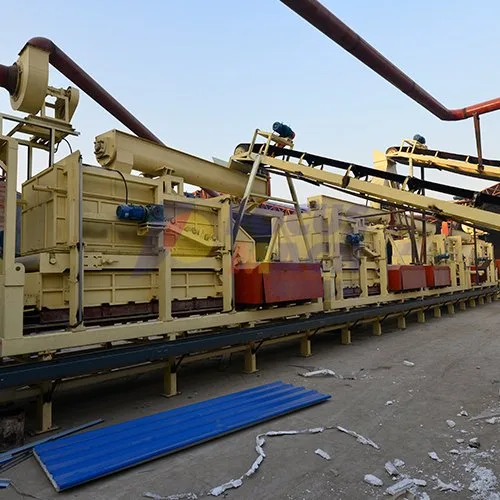
Surface and core flakes are processed separately. Wood flakes are metered out from a silo, passed through a vibrating feeder, and continuously weighed by a dosing device before being fed into a ring-type glue mixer. The mixer thoroughly blends the wood flakes with atomized adhesive, ensuring uniform coating. The amount of adhesive applied is automatically adjusted in response to fluctuations in the wood flake feed rate, maintaining a constant resin-to-wood ratio as defined by the process requirements.
5 · Hot-Pressing Section
After the adhesive is applied, the surface and core wood chips are transported via a belt conveyor to a mobile pneumatic forming station. Two sets of opposing air-jet nozzles distribute the chips. On the mesh belt of the forming conveyor, the material is laid down to create a particleboard structure with fine, uniform outer layers and a graded internal composition. The formed particleboard mat is cut to the required length by a cross-cut saw, and the offcuts are returned to the forming station via an air-conveying system. During the hot-pressing process, the forming conveyor simultaneously moves the pressed board out of the press while feeding a new mat into it. Meanwhile, the forming station moves rapidly in the same direction, laying down a new mat once it reaches the starting position. Any substandard boards can be sent back to the wet-material bin for recycling.
6 · Edge-Sawing Section
The pressed raw board (mat) moves onto a conveyor equipped with a weighing system, where it is centered and weighed. It then enters a longitudinal and transverse sawing machine, where it is trimmed to the final dimensions. The resulting offcuts can also be returned to the wet-material bin. The trimmed boards are moved via a roller conveyor—passing through a centering device—to a stacking area with a hydraulic lifting platform. From there, they are transferred to a roller-bed staging area, where a forklift collects them for transport to the intermediate storage zone. 7 · Sanding Section
The stored boards are fed into the sanding system. The sanding system consists of a hydraulic lifting platform, a roller conveyor, a wide-belt sander, and other components. Once sanded, the finished boards undergo inspection and classification before being moved to the finished-product warehouse.
8 · Electrical Control System
The particleboard production line features a central control station that oversees the entire process—from particle metering, calibration, and forming to hot pressing and final edge-trim weighing. The line can be operated either automatically or manually, governed by a pre-programmed PLC system. Additionally, local control stations (cabinets) are installed at each operational section—with the exception of the forming and hot-pressing sections—to manage and monitor the equipment within those specific areas.