 86-539-3101518
Fax: 86-539-3101518
Mobile: +86-15969943322
+86-18853986768
Email: Jasonqiao@sdfocusmachinery.com
Factory address: No.1 Zhubao wood industry zone, Lanshan district, Linyi-276000, Shandong,China.
Office: F16, Amethyst mansion, Linyi, Shandong,China.
Time: 2026-10-19 14:41
Description:

 Jasonqiao@sdfocusmachinery.com
Product Details
Brief Introduction to OSB / PB Production Line
Brief Production Process Description
1. Wood Chipping Preparation Section
Wood raw materials are delivered to the factory and stored separately according to tree species.
Option 1: Logs, branches and other short materials are conveyed by belt conveyor to the drum chipper. Qualified wood chips cut by the chipper are transported to the wood chip silo for intermediate storage via discharge belt conveyor and bucket elevator. The wood chips are processed into high-quality wood strands by a ring flaker, then pneumatically conveyed to the wet strand bin.
Option 2: Wood raw materials are fed by feeding conveyor into the long log flaker, and cut into qualified strands in one pass. The strands are pneumatically sent to the wet strand bin.
Option 3: Long wood such as small-diameter logs is fed by feeding conveyor into the long log flaker and cut into qualified wood strands in one pass. The strands are pneumatically delivered to the wet shaving silo. Logs, branches and other short materials are transported by belt conveyor to the drum chipper. Qualified wood chips cut by the chipper are pneumatically sent to the silo for intermediate storage. The wood chips are made into high-quality wood strands by ring flaker and blown to the wet strand bin by air flow.
2. Drying and Sorting Section
Strands discharged from the wet material bin are fed into the rotary dryer through screw conveyor. The dried strands are then sent by screw conveyor to the screening machine for classification. The dryer discharge screw conveyor is equipped with a spark detection device. Once the alarm signal is triggered, dry materials can be automatically discharged from the system. Oversized strands after screening go to the re-crusher for further processing. Together with medium-sized screened strands, they are transported by screw conveyor to the air classifier for sorting. Qualified fine materials from screening are sent to the strand bin. Qualified materials separated by air classifier are delivered to the strand silo for intermediate storage. Oversized materials sorted out are crushed in the grinder, combined with fine screened strands and fed into the strand bin. According to different proportion requirements of surface layer and core layer strands for boards of different thickness, coarse strands can be quantitatively transported to the grinding machine to produce fine surface strands.
3. Glue Preparation Section
This section covers preparation and delivery of paraffin emulsion and hardener solution, additive storage, as well as mixed glue batching and application system. Mixed glue for surface layer and core layer is prepared in the centralized glue mixing unit. The mixed glue batching and application system adopts PLC program control. It can realize automatic metering, continuous batching, quantitative gluing and adjustment in accordance with process specifications.
4. Forming Preparation Section
Surface and core strands are glued separately. Wood strands are quantitatively discharged from the silo, pass through the vibratory feeder and continuously weighed by the dosing unit, then evenly fed into the ring glue blender. The glue blender fully mixes the incoming wood strands and sprayed glue liquid, achieving uniform glue coating. It automatically adjusts glue application volume according to the fluctuation of strand feeding rate to maintain the constant glue ratio required by the process.
5. Hot Pressing Section
After gluing, surface and core strands are transported by belt conveyor to the mobile pneumatic forming machine. Two sets of opposite air nozzles blow and spread the strands. On the mesh belt of forming conveyor, thin and uniform layers are formed on top and bottom, creating the gradient structure of particle board. The formed particle board mat is cut to required length by cross-cut saw, and the trimmings are returned to the forming machine via pneumatic conveying system. After single-layer hot press operation, the forming conveyor simultaneously moves finished boards out of the press and feeds new mat into the press. Meanwhile the forming machine moves rapidly in the same direction. When stationary, a new mat is laid. Unqualified boards can be sent back to the wet bin for recycling through the recycling device.
6. Edge Trimming Saw Section
Pressed raw boards enter the weighing conveyor, for centering and weighing. Centered and weighed raw boards go into the longitudinal and cross cutting saw, cutting the raw boards into finished size. Trimming waste can also be returned to the wet waste bin. Trimmed boards are conveyed by roller conveyor through centering device to the stacking station and hydraulic lifting platform, then transferred to forklift roller platform and delivered to intermediate storage by forklift.
7. Sanding Section
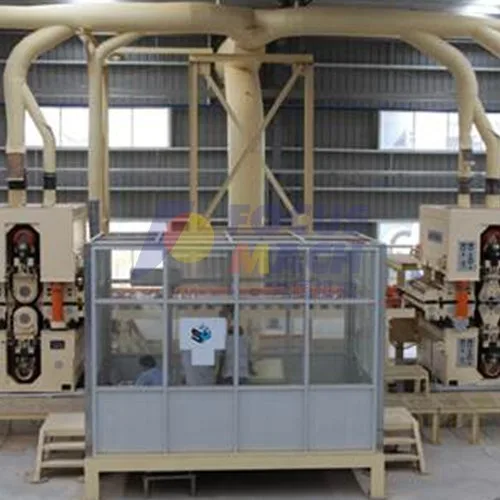
Stored boards are sent to the sanding system. The sanding system consists of hydraulic lifting platform, roller conveyor, wide-belt sander and other equipment. After sanding, finished boards go through inspection and grading before entering the finished product warehouse.
8. Electric Control System
The particle board production line is equipped with a main control room. From board weighing, calibration, forming, hot pressing to full-edge trimming, the whole line can run automatically or manually under PLC programmed control. Besides, local operation stations (control boxes) are installed at each section (except forming and hot pressing section) to monitor and control the equipment of corresponding section.